AQL Inspection for Insulated Bags: Extra Checks Beyond General Merchandise
Sampling alone does not tell you whether an insulated unit will hold temperature, and it certainly does not tell you whether the liner will leak. Those sit outside the general attribute list. This article covers the additional checks an insulated construction needs, and what each one is worth.
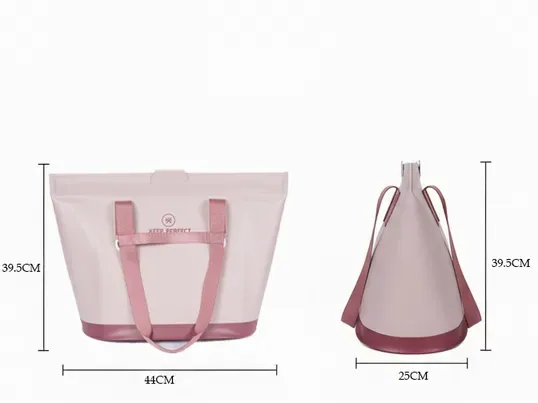
Add five things to the general list: liner integrity at the welds, leak behaviour under a stated fill, insulation thickness and recovery, cold-conditioned flexibility, and the food contact evidence for the destination market.
An insulated bag fails differently from a plain one. Its purpose is measurable — keep the contents cold or warm for a stated period — and its construction includes a layer that cannot be repaired once made. A fault that would be a nuisance in a general product can make an insulated unit unfit for the only job it was bought to do.
Yet the additional exposure is rarely reflected in the inspection brief. The checklist used for a plain unit is applied unchanged, the finding for any insulated-specific fault is recorded under something generic, and six weeks later a customer discovers the liner separated at a corner nobody thought to examine.
What Makes an Insulated Unit Different?
Three things. It contains a welded film liner whose integrity cannot be verified after closing and cannot be repaired at all. It depends on an insulation layer whose performance is a function of thickness and recovery rather than of appearance. And it is often used in contact with food, which adds an evidential requirement none of the others carry.
Together these mean that several important attributes cannot be assessed by looking at finished units alone. They need a check that was designed for them, run at a point in the process where the result is still informative.
Which Checks Sit Outside a General Merchandise Checklist?
Eight additions cover most of the exposure, and none of them takes long. The difficulty is not effort; it is remembering to specify them before the booking rather than after the report.
| Extra check | What the inspector does | What establishes a pass | Why it earns its place |
|---|---|---|---|
| Liner weld integrity | Every weld examined under good light, with gentle opposing pull at corners | No separation, thinning or pinholing beyond the stated amount | A liner cannot be repaired; one split ends the product |
| Leak behaviour | Liner filled with water to a stated level, rested, and turned through stated positions | No moisture passing the liner or its welds | The failure customers discover first, and always at the worst moment |
| Insulation thickness and recovery | Thickness measured at stated points before and after a stated compression period | Within the stated range, and recovery beyond the stated minimum | Two materials can measure identical and perform very differently |
| Closure performance when cold | Liner closure worked after conditioning to a stated temperature | Sealing and releasing normally at that temperature | Materials stiffen in the cold; units are used cold |
| Cold-conditioned flex | Panel flexed after conditioning to a stated temperature | No cracking, no delamination, no audible creak | The corner case that produces warranty claims in northern markets |
| Condensation behaviour | Unit filled cold, rested in stated conditions and examined | No internal wetting beyond what the construction intends | A surprising source of complaints that read as leakage |
| Food contact evidence | Documentation checked against the destination market requirement | A valid report covering the liner and any printed surface | An evidential requirement rather than a quality one |
| Odour assessment | Unit opened and assessed after a stated interval with the closure sealed | Below the agreed threshold | Odour complaints are disproportionate to their cost to fix |
How Should a Welded Liner Be Examined?
Under strong light, from both sides, with the panel flexed rather than lying flat. A weld that looks intact lying still can show a thin line of separation when flexed gently, and that line is what becomes a leak in service. Work systematically along every weld rather than looking generally at the interior.
Pay particular attention to corners and to where the liner meets the closure. Corners concentrate stress because two welds meet there; the closure junction combines a sealed joint with whatever strain the closure applies. Both deserve deliberate attention on every unit in the sample rather than on the first one.
Pinhole detection deserves its own mention. Very small openings along a weld are invisible to the eye and consequential in use. Where the programme is sensitive, specify a method — filling the liner and observing under a stated pressure or duration — rather than relying on inspection to notice them.
How Do You Check Thermal Performance Without a Laboratory?
You can measure something useful, though not everything. A controlled test — stated fill, stated starting temperature, stated ambient conditions, stated duration, then a reading — produces a comparative figure you can hold future lots against. It is not an accredited result, and it should never be presented as one.
Where a figure will be published or relied on contractually, it must come from a laboratory using a recognised thermal transmission method. Those results depend on apparatus, conditioning and method in ways a floor test cannot replicate, and presenting a shop-floor reading as if it were equivalent is how programmes lose arguments they should have won.
Use the floor version for its real purpose: detecting drift. A lot performing noticeably worse than the last one is worth investigating even if both are formally acceptable, because that divergence usually has a cause.
What Does a Leak Check Involve?
A stated volume of water in the liner, a stated rest period, then a stated sequence of positions — upright, inverted, on each side, and finally with gentle pressure applied. Record which position produced evidence and where. A leak that appears only inverted tells you where the fault is; one that appears immediately usually tells you it is large.
Do this on units drawn from production rather than on a convenient spare, and say how many. Three is a reasonable number where destructive testing is not required and more where leakage risk is high, and the units should be identified so their position in the lot is known.
How Is Insulation Thickness and Recovery Checked?
With a calliper at a stated pressure, at stated points, before and after a stated compression. The second reading is the informative one: a material that compresses and fails to recover has lost the property the product depends on, however well it measures before.
State the recovery interval. Some foams recover within minutes and others take hours, and comparing materials measured at different points produces readings that mean nothing. Say how long, and hold everybody to it.
| Failure seen | Where it appears | Likely cause | Consequence for the unit |
|---|---|---|---|
| Weld separation at a corner | Interior corners of the liner | Insufficient weld width or contamination in the weld area | Terminal — the liner cannot be repaired |
| Pinholes along a weld | Any weld line | Weld parameter drift during the run | Slow leakage that looks like condensation |
| Insulation not recovering | Base, corners and under handles | Density too low for the duty, or compressed for too long | Performance falls without any visible change |
| Delamination of the liner from the shell | Large panels | Adhesive not suited to the substrate, or inadequate cure | Progressive; gets worse rather than staying put |
| Closure stiff when cold | Liner closure or any sealed opening | Material selection for the temperature range | The customer cannot seal the unit when using it |
| Internal wetting | Inside the outer shell | Condensation rather than leakage, which matters for the fix | Often misreported as leakage by customers |
How Does Food Contact Evidence Fit In?
As documentation rather than as inspection. Where the liner, the printed surfaces or any component contacts food in the destination market, there is normally a requirement for evidence of suitability, and that evidence is a laboratory report dated within its validity.
Check three things on every such report: that it covers the actual material rather than a similar one, that the destination market is the one named, and that the date still holds. Reports satisfying two of those are extremely common and worth approximately nothing.
How Should Findings Be Classed Here?
Harsher than general merchandise, and deliberately. Anything compromising the liner is normally a major, because the unit cannot do what it was bought for and cannot be repaired. Performance below a stated minimum is a major for the same reason. Missing or invalid food contact documentation is treated separately, because it is a compliance exposure rather than an attribute finding.
One boundary deserves agreement in advance: cosmetic faults on external panels of an insulated unit. These usually stay minor, as elsewhere. It is worth confirming rather than assuming, because the presence of the liner changes how some buyers read everything else about the unit.
What Belongs in the Insulated Clause?
Ten additions to the clause for an insulated construction
- Liner material, thickness and the welding method.
- The weld examination method, including flexing under stated light.
- The leak check: volume, rest period, positions, how many units.
- Insulation thickness, the measurement pressure and stated points.
- Recovery requirement and the interval after which it is read.
- Conditioning temperature for any cold-flex assessment.
- Thermal performance comparison method for floor testing.
- Which laboratory method governs any published performance figure.
- Food contact documentation for the named destination market.
- The defect class for each insulated-specific failure.
Write these once and they serve the whole range. Rather more usefully, they let two constructions be compared honestly for the first time, because otherwise the comparison is between one supplier's claims and another's.
Does the Liner Change How the Sampling Plan Applies?
It changes where it applies rather than how. The general plan still governs the attribute counts on drawn units, and those counts still mean what they mean. What the liner adds is a set of attributes that only exist on this construction, which the general defect list does not mention and therefore cannot find.
Write them as additional entries in the same classification rather than as a separate document with separate rules. A second list with its own classes invites exactly the confusion this whole exercise is meant to remove — two sets of counts, two sets of thresholds, and no way to combine them.
What Should Be Checked Before the Liner Is Closed In?
Everything that becomes invisible afterwards. Once the liner is inside the shell and the closing operation is done, weld integrity can only be assessed indirectly, insulation compression becomes harder to attribute, and nothing can be repaired. That argues for looking while assembly is still open.
In practice this means an early look rather than a late one: the first liner assemblies examined while that operation is running, rather than waiting for finished units to exist. It takes little time and it is the last point at which anything found can still be addressed without waste.
Ask specifically whether units were extracted and re-closed during development. A liner that passed a repair during sampling will not behave the same as one made cleanly, and using repaired units as reference samples distorts everything after them.
Sampling takes 6-10 working days from a signed-off tech pack, and this is the point where insulated-specific requirements belong. Decisions made later than the approval — which liner material, which closure behaviour, which market the evidence must cover — are decisions that cannot be undone once bulk starts.
What Does a Sample Approve for an Insulated Unit?
More than its appearance. Approving an insulated sample implicitly accepts the liner material, the welding method, the insulation density and thickness, the closure arrangement and whatever evidence accompanies them. If any of those was never discussed, approval is still usually read as accepting them.
Mark it explicitly. A short statement alongside the approval — that performance is subject to the stated checks and to valid market evidence — keeps the conversation open without weakening the approval itself, and it prevents the later awkwardness of discovering what everybody assumed was agreed.
How Does Cold Chain Duty Change the Specification?
The duty determines nearly everything else. Holding temperature for a few hours while goods are carried differs entirely from an overnight hold or a regulated distribution use, and specifying one while selling the other is a consistent source of disappointment that nobody remembers agreeing to.
Write the intended duty into the specification as a stated fill, stated starting condition, stated ambient and stated period. Those four numbers make every later discussion concrete and remove the drift that occurs when everybody retains their own idea of the requirement.
Why Does This Sit Beside Rather Than Inside the General Plan?
Because the sampling plan governs attributes, and these checks govern performance. Drawing 50 units at AQL 2.5 is the right way to establish that the lot meets the general attribute requirements; it says nothing about whether the liner holds water. Both are needed, and they are not substitutes.
Run them on units drawn within the sample where they are non-destructive, and on separate units where they are not. Either way, record which units were tested, because a performance finding attached to an unidentified unit cannot be traced to anything.
What Changes Across a Repeat Programme?
Insulated constructions drift more than plain ones, because there are more parameters to drift. Weld settings, adhesive batches, foam lots and lining thickness all move slowly, and none of the movement is visible in an attribute count. A repeat that looks clean can be measurably worse than the lot it came from.
Keep the floor comparison figures — the ones nobody publishes — precisely for this. They are the record that lets you notice a slow decline before it reaches the point where a customer does.
How Should Sensible Limits Be Recorded?
Alongside the failure counts rather than separately. An insulated-specific finding is still a finding under the plan, and recording it somewhere else is how the same lot gets counted in two places and understood in neither.
Where a check is destructive or expensive, say how many units and how the result extrapolates. Three units leaking none of them means something different from ten units leaking none of them, and the report should make that difference legible without the reader having to ask.
Keep the food contact evidence with the lot record rather than in a compliance folder elsewhere. When somebody asks, the answer should take seconds, because the question always arrives when nobody has time for it.
Add the insulated checks to your brief
Share the construction and its liner specification — weld, leak, recovery and evidence requirements come back written into the checklist.
Frequently Asked Questions
Can an insulated bag be inspected with a general checklist?
It can be inspected for attributes, yes — the performance checks are additional and need their own lines in the brief.
How many units should be leak tested?
Three of the sample is a common starting point, more where the risk is judged high, always drawn from production and identified.
What causes a liner weld to separate?
Usually insufficient weld width or contamination in the weld area. Process parameter drift during a run produces it progressively.
Can thermal performance be measured on the floor?
A comparative figure can, yes. Any published or contractual figure must come from a laboratory using a recognised transmission method.
Why does insulation lose performance without looking different?
Because performance depends on recovered thickness. Compressed material that does not spring back measures badly but looks unchanged.
Are external cosmetic faults still minor on insulated units?
Usually yes. Confirm it in the clause rather than assuming, because the liner changes how outsiders read the rest of the unit.
When should the leak check be run?
On finished production units, before packing, so failures are found while replacement is still possible.
What documentation does a food liner need?
Evidence of suitability for food contact in the named destination market, valid at the date relied on, covering the actual material used.
How is a cold-flex check performed?
Condition the unit to a stated temperature, flex the panel, and look for cracking, delamination or audible creaking.
Why do customers report condensation as leakage?
Because both present as internal wetting. Establishing which it is determines whether the fix is in construction or in ventilation.
Should pinhole checks be specified?
Where leakage risk matters, yes — a stated method finds small openings the eye cannot.
Where do liners most often fail?
At interior corners where two welds meet, and where the liner joins the closure.
Does a longer cold hold always mean better insulation?
No. It depends on thickness, density, recovery and closure integrity together, any one of which can govern.
People Also Ask
What extra checks does an insulated bag need?
Liner weld integrity, leak behaviour, insulation thickness and recovery, cold-conditioned flexibility, odour, and food contact documentation.
How do you test a cooler bag liner?
Examine every weld under light with the panel flexed, then fill to a stated level, rest, turn through stated positions and look for moisture.
Can cooler bag insulation be checked without a laboratory?
A comparative figure can be produced on the floor. Published figures need a laboratory method.
Why does my cooler bag leak?
Usually a weld that separated at a corner, or pinholes along a weld line. Both are invisible from outside.
What makes insulation stop working?
Loss of recovered thickness. Compressed material that does not spring back performs badly while looking unchanged.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ASTM C518 — Steady-state thermal transmission propertiesASTM International
- ASTM International — standards indexASTM International
- ISO 2859-1:1999 Sampling procedures for inspection by attributesInternational Organization for Standardization